
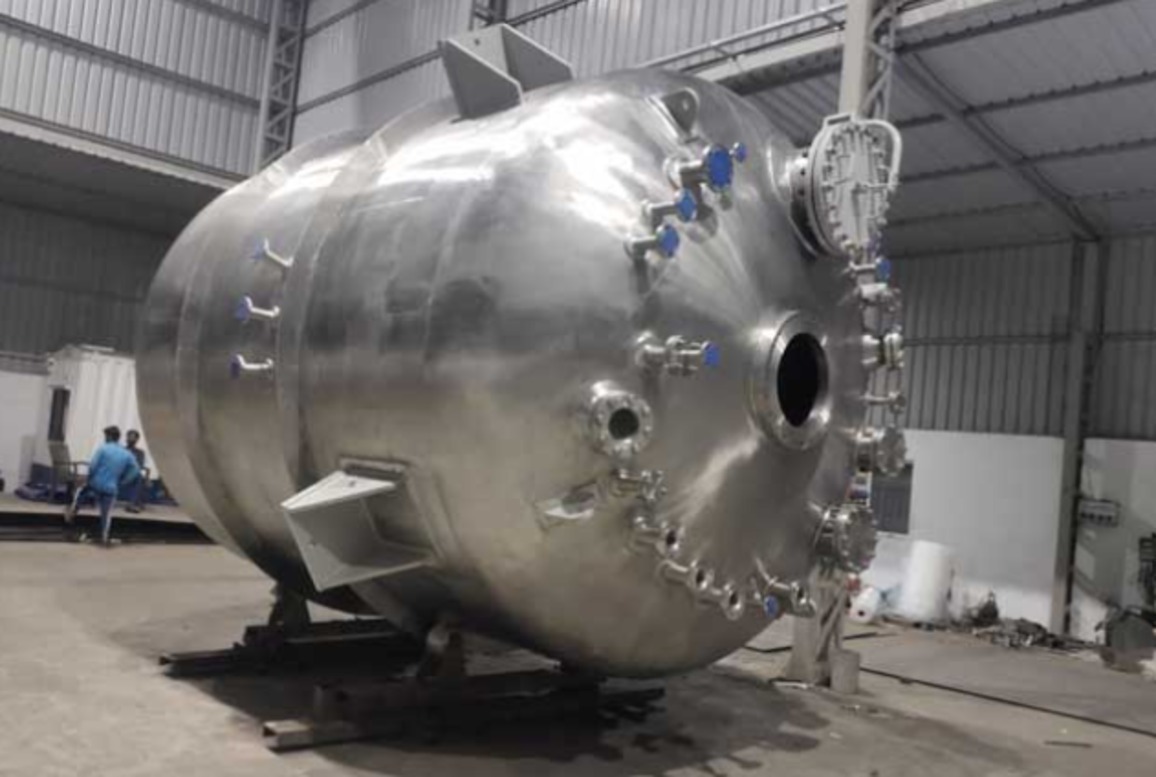
Chemical processing industries depend on accurate reaction control, reliable equipment design, and safe operating conditions to achieve consistent production results. The reactor is one of the most important components in any chemical manufacturing facility because it provides the controlled environment required for chemical reactions.
A Chemical Reactor Manufacturer in Pune designs reactor systems based on process requirements such as temperature control, pressure conditions, chemical compatibility, and production capacity. With Pune becoming a significant industrial and manufacturing hub in Maharashtra, chemical companies require dependable reactor solutions that support efficient and safe operations.
Understanding The Role Of Chemical Reactors
A chemical reactor is an engineered vessel where chemical reactions take place under controlled conditions. The design of the reactor influences reaction efficiency, product quality, and operational safety.
Chemical reactors help manufacturers control:
Reaction temperature
Mixing efficiency
Pressure levels
Residence time
Material interaction
A well-designed reactor ensures that chemical processes occur consistently while reducing production challenges.
Types Of Chemical Reactors Used In Industries
Different chemical applications require different reactor configurations.
Stainless Steel Reactors
Stainless steel reactors are commonly used because of their corrosion resistance and durability. They are suitable for industries handling different chemicals and formulations.
Pressure Reactors
Pressure reactors are designed for processes requiring controlled pressure conditions. They are used where reactions cannot be performed effectively under atmospheric conditions.
Agitated Reactors
Agitated reactors use mechanical mixing systems to maintain uniform distribution of materials and improve reaction performance.
Jacketed Reactors
Jacketed reactors provide heating and cooling capabilities, making them suitable for reactions requiring precise temperature management.
Factors To Consider When Choosing A Chemical Reactor
Selecting the right reactor requires detailed evaluation of the manufacturing process.
Important factors include:
Chemical Compatibility
The vessel material must be compatible with the chemicals being processed. Incorrect material selection can lead to corrosion, contamination, and reduced equipment life.
Operating Conditions
Temperature, pressure, and reaction characteristics influence reactor design.
Mixing Requirements
Different chemical processes require different agitation speeds and mixing patterns.
Production Capacity
The reactor size should match current production needs while allowing future scalability.
Safety Considerations
Proper pressure ratings, safety controls, and engineering standards are essential for chemical processing applications.
Applications Of Chemical Reactors
Chemical reactors are used in:
Specialty chemical production
Pharmaceutical intermediates
Agrochemical manufacturing
Resin production
Polymer processing
Industrial chemical synthesis
Each application requires customized equipment design based on the nature of the process.
Importance Of Quality Reactor Fabrication
Reactor fabrication requires engineering accuracy, quality materials, and manufacturing expertise. Weld quality, surface finish, dimensional accuracy, and testing procedures directly affect long-term performance.
Nes India Engineers provides process equipment solutions including chemical reactors, storage tanks, mixing systems, and industrial vessels. The company develops equipment based on industry requirements and operational conditions.
For chemical manufacturers in Pune and across Maharashtra, selecting the right reactor system helps improve process reliability, enhance safety, and maintain consistent production quality.